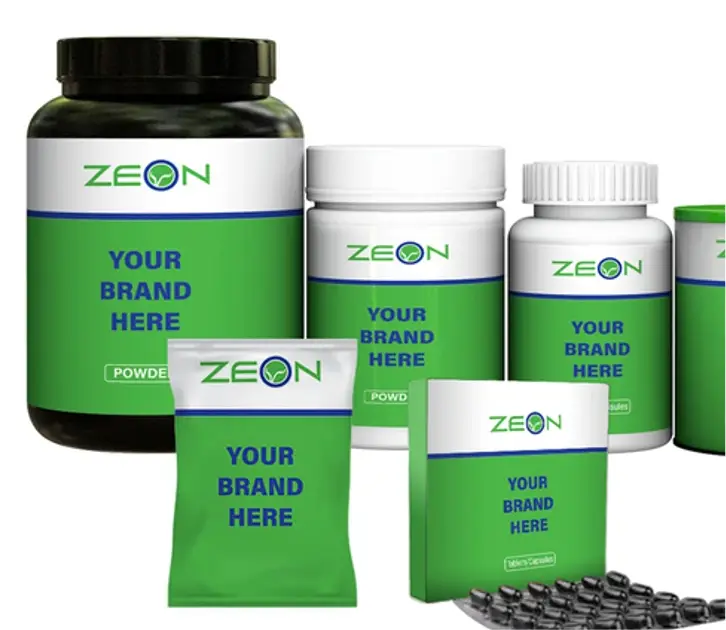
CE Certified Supplement Packaging Manufacturer & Factories
Precision-Engineered Primary & Secondary Packaging Architecture, Advanced Barrier Protection, and Contract Manufacturing Excellence for Global Healthcare Brands.
Export-Grade Product Line
CE Certified Supplement Packaging Solutions
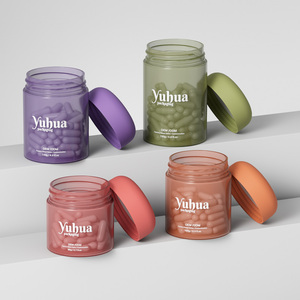
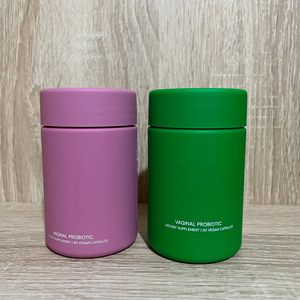
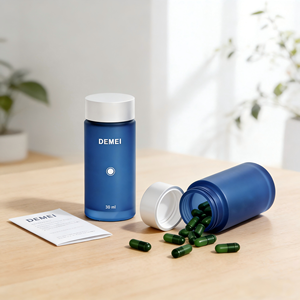
Explore our validated range of high-barrier containers, bottles, effervescent tubes, and rigid luxury boxes engineered for global nutraceutical compliance.
38+ Years of Contract Manufacturing & Packaging Supremacy
Operating from state-of-the-art facilities compliant with US FDA, FSSC 22000, ISO 15378, and European CE directives.
38+
Years Manufacturing Legacy
850+
Commercialized SKUs
60+
Global Export Markets
400M
Annual Tablet Capacity
35K MT
Powder Blending Output
Technical Whitepaper & Engineering Guide
CE Certified Packaging Architecture for Modern Dietary Supplements
An authoritative analysis of regulatory compliance, polymer barrier technology, degradation prevention, and global supply chain risk mitigation.
1. The Strategic Imperative of CE Certification & ISO 15378 in Primary Packaging
In the highly regulated global nutraceutical and dietary supplement ecosystem, primary packaging serves as far more than a brand canvas—it functions as a critical protective barrier that preserves bio-potency, guarantees chemical stability, and ensures consumer safety. As regulatory scrutiny increases across the European Union (under EU Regulation 2017/745 for combined health devices and Regulation EU 10/2011 for Food Contact Materials), supplement brand owners cannot afford compromised packaging integrity.
Our manufacturing matrix operates at the intersection of European CE compliance and ISO 15378 (Primary Packaging Materials for Medicinal Products). Achieving CE certification for supplement packaging requires strict adherence to non-toxicity, chemical inertness, heavy metal limits (RoHS compliance), and structural safety under environmental stress. By integrating automated vision inspection systems and cleanroom moulding facilities (Class 8 environment), our factories eliminate particulate contamination, pinhole flaws, and volatile organic compound (VOC) off-gassing, guaranteeing that every jar, bottle, and tube meets rigorous international pharmacopeial standards.
Selecting the optimal container material requires a precise understanding of Water Vapor Transmission Rates (WVTR), Oxygen Transmission Rates (OTR), light-transmittance protection, and mechanical tensile endurance. The table below outlines the engineered parameters of our CE-certified packaging materials:
Our integrated manufacturing plants combine raw material polymer synthesis, injection blow moulding, and custom surface treatment within a unified quality framework:
Precision Desiccant Closure Technology
Effervescent tablets and hygroscopic botanical powders degrade rapidly under relative humidity exceeding 40%. Our PP effervescent tubes feature spiral-spring stoppers integrated with molecular sieve silica gel, guaranteeing active ingredient potency throughout a 36-month shelf life.
CRSF (Child-Resistant Senior-Friendly) Seals
Balancing European compliance for child resistance with senior accessibility, our push-and-turn closures utilize multi-lead continuous threads and induction heat-seal aluminum foils to deliver tamper-evident protection and zero leakage during transatlantic transport.
Spectrophotometric Light Blocking
Certain bioactive molecules—such as Vitamin B12, CoQ10, and Curcumin—are prone to photodegradation. Our amber PET and frosted glass lines filter out UV radiation wavelengths between 290nm and 450nm, safeguarding formulation stability.
Strategic Sourcing Intelligence
Future Procurement Trends in Supplement Packaging (2025–2030)
How forward-thinking health brands are navigating eco-regulations, smart authentication, and tactile consumer engagement.
1. Transition to Post-Consumer Recycled (PCR) Polymers & Circular Systems
Global procurement teams are heavily prioritizing PCR PET and ocean-bound plastic resins to meet strict European packaging waste levies. Our factories now supply up to 100% food-contact approved PCR plastic options that retain mechanical strength while slashing brand carbon footprints by over 45%.
Information Gain Key Insight: PCR resins processed under cleanroom conditions prevent chemical migration, ensuring full compliance with EU food contact standards.
With global D2C cross-border sales expanding rapidly, brand protection is critical. Modern packaging now incorporates hidden micro-code printing, tamper-evident security holographic seals, and integrated NFC tags. This empowers consumers to verify product authenticity directly with their smartphones while granting brands real-time supply chain traceability.
3. Unboxing Experience & Tactile Premiumization in D2C Channels
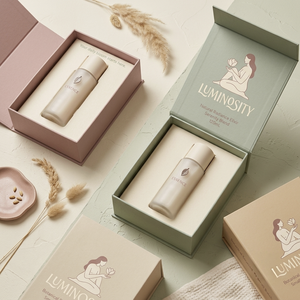
The rise of premium subscription boxes for anti-aging NMN, longevity collagen powders, and personalized nutrition has elevated secondary packaging. Matte soft-touch coatings, custom magnetic rigid presentation boxes, and embossed metallic detailing generate viral unboxing moments that increase customer retention and brand equity.
The Manufacturer's Edge
Why Top Pharmaceutical & Wellness Brands Partner With Us
Combining rigorous instrumented quality control with scalable economic efficiency for over three decades.
In-House Analytical Laboratory
Every raw polymer batch undergoes Gas Chromatography (GC), Differential Scanning Calorimetry (DSC), and heavy metal spectroscopy to guarantee absolute purity before production begins.
Full Regulatory Dossier Support
We provide full technical documentation—including Certificates of Analysis (COA), Food Contact Statements, Halal certificates, and Stability Test summaries—for seamless global customs clearance.
Custom Tooling & Rapid Prototyping
Our dedicated CAD/CAM engineers take your proprietary bottle concept from initial 3D design to functional prototype sampling within 10 to 14 business days.
Procurement & Technical FAQ
Frequently Asked Questions by B2B Procurement Teams
Clear, direct answers regarding minimum order quantities, compliance protocols, testing, and production lead times.
Our CE certified supplement packaging adheres directly to European Union Directives for plastic materials intended to come into contact with food (EU Regulation 10/2011) and heavy metal threshold limits under RoHS guidelines. Additionally, our cleanroom manufacturing protocols conform to ISO 15378, ensuring complete batch traceability, non-toxicity, and chemical inertness under rigorous extraction testing.
Our PP effervescent cylinder containers feature a specialized closure system equipped with an integrated desiccant chamber filled with active silica gel or molecular sieves. Coupled with an ultra-low WVTR polypropylene body and airtight spiral stoppers, this system maintains relative humidity inside the tube below critical degradation levels, extending effervescent tablet shelf life.
For standard catalog items (such as HDPE bottles or PET jars in standard colors), MOQs start as low as 10,000 units. For custom-moulded shapes, unique color matching, or specialized soft-touch coatings, MOQs typically range from 20,000 to 50,000 units. Standard production lead times are 3 to 4 weeks following final artwork and sample approval.
Yes. Our in-house engineering team provides complete end-to-end OEM/ODM services, including 3D mechanical rendering, rapid SLA prototype printing, mold tool manufacturing, and full pilot-run batch validation. Custom tooling typically takes 15 to 25 days depending on design complexity.
Absolute integrity is guaranteed through rigorous leak testing under negative pressure vacuum chambers (-0.08 MPa). When paired with properly calibrated induction heat-foil liners and continuous-thread closures, our packaging maintains zero leakage despite atmospheric pressure changes during air transportation or prolonged ocean shipping.
Ready to Upgrade Your Supplement Packaging Sourcing?
Connect directly with our technical engineering team to request sample kits, request custom mould feasibility studies, or download our complete product specs catalog.