Engineered for high bioavailability, exceptional micro-homogeneity, and long-term storage stability across feed, nutraceutical, and food beverage applications.
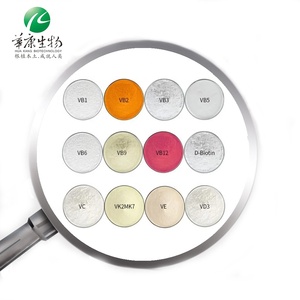
In the modern global food, beverage, nutraceutical, and animal nutrition supply chains, custom vitamin premixes serve as essential micronutrient delivery vectors. Rather than procuring isolated fat-soluble and water-soluble vitamins individually—which introduces significant batch-to-batch micro-dosing error risks and operational inefficiencies—global procurement directors and formulators increasingly rely on specialized B2B vitamin premix manufacturers in China. China produces over 70% of the world's primary vitamins (including Vitamin C, B-Complex, Vitamin E, and Vitamin A derivatives), making its advanced premix compounding plants the global nexus for cost-efficient, audit-ready, high-homogeneity micronutrient blends.
Achieving uniform micro-dispersion in bulk premixes requires sophisticated industrial particle engineering. When mixing trace active ingredients (such as Folic Acid, Vitamin B12, or Biotin) operating at concentrations as low as parts-per-million (PPM) alongside macro-carriers (such as corn cob meal, maltodextrin, or calcium carbonate), standard ribbon blenders fail. Leading Chinese manufacturers leverage multi-axial fluidizing micro-blenders, spray-granulation micro-encapsulation, and strict Coefficient of Variation (CV < 5%) validation protocols to ensure each grain of final product contains identical nutritional ratios.
Advanced lipid and hydrocolloid beadlet matrix protection prevents oxidative degradation of fat-soluble vitamins (A, D3, E, K3) during heat processing, pelleting, and prolonged shelf storage.
Rigorous HPLC batch testing ensures a Coefficient of Variation (CV) under 5%, guaranteeing strict regulatory compliance, eliminating toxic hot-spots, and preventing nutrient deficiencies.
Full international regulatory compliance packages including US FDA registration, FSSC 22000, ISO 22000, GMP, HACCP, FSSAI, AYUSH, and Halal certification for frictionless export.
Comprehensive formulation parameters tailored to specific industrial end-uses.
| Application Category | Target Active Ingredients | Carrier & Excipient System | Key Performance Metrics | Compliance Standard |
|---|---|---|---|---|
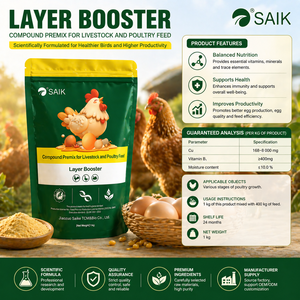
| Poultry & Layer Boosters | Vit A, D3, E, K3, B-Complex, Lysine, Methionine | Defatted Rice Bran / Fine Corn Cob (40-60 mesh) | CV < 3.8% High Heat Resistance | Feed Grade (FAMI-QS / GMP+) |
| Swine Anti-Stress Premix | Vit B1, B2, B3 (Niacin), B6, Vitamin C, Organic Zinc | Silicon Dioxide / Corn Cob Meal | Anti-hygroscopic, Free-flowing | Feed Grade ISO 22000 |
| Energy Drink & Beverage | Ascorbic Acid, Niacinamide, B6, B12, Folic Acid | Maltodextrin / Water-soluble Dextrose | 100% Water Soluble High Clarity | Food Grade / US FDA / FSSC 22000 |
| Ruminant Bio-Enzyme Premix | Fat-soluble Vit A/D/E, Choline Chloride, Rumen Enzymes | Coarse Corn Cob (20-40 mesh) / Calcium Carbonate | Rumen-bypass micro-encapsulation | Feed Grade / Halal Certified |
| Nutraceutical Tablets & Capsules | High-Potency Multivitamin & Mineral Complex | Microcrystalline Cellulose (MCC 102) / Silica | Direct Compression Ready (DC Grade) | USP / EP / FSSAI Compliant |
As global supply chains shift toward heightened traceability, stringent environmental impact metrics, and hyper-personalized nutrition, the procurement landscape for B2B vitamin premixes is undergoing a fundamental transformation. Sourcing directors must anticipate key macro-trends to secure resilient supply contracts:
Traditional chemical synthesis of vitamins (such as Vitamin E and B-complex) is rapidly giving way to precision microbial fermentation. China’s leading manufacturers are integrating synthetic biology platforms to produce green, zero-carbon vitamin actives that meet strict EU CBAM and ESG mandates while delivering higher biological purity.
Industrial scale-up demands zero margin for human error. Modern Chinese premix plants utilize fully enclosed automated micro-dosing systems equipped with inline Near-Infrared (NIR) spectroscopy. This technology monitors blend homogeneity in real time during batch mixing, automatically stopping the process only when optimal particle distribution is mathematically proven.
Global demand is splitting sharply between animal feed carriers (cost-optimized defatted rice bran and non-GMO corn cob meal) and food-grade hypoallergenic carriers (organic tapioca maltodextrin, rice starch, and soluble acacia gum). Premix suppliers offering flexible carrier swap protocols without cross-contamination are gaining decisive market share.
Water-soluble beverages and liquid feed supplements suffer from rapid oxidation of sensitive vitamins like C, B1, and A. The future of high-value premix manufacturing lies in cold-water-dispersible (CWD) micro-emulsions and spray-dried liposomal powders that shield active molecules from light, oxygen, and pH shifts.
Building on nearly four decades of formulation leadership, our integrated manufacturing campus delivers end-to-end reliability for global brand owners.
Equipped with state-of-the-art High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC), Atomic Absorption Spectroscopy (AAS), and rapid microbiology testing to validate potency, heavy metals, and stability for every batch.
Our dedicated regulatory logistics division handles complete export documentation packs—including Certificates of Free Sale, GMP Certificates, COAs, Allergen Declarations, and custom shipping-mark compliance—ensuring smooth customs clearance worldwide.
Our pilot R&D trial mixers mirror full-scale production line dynamics. Formulations developed in our pilot lab scale seamlessly up to 35,000 MT commercial batches without requiring excipient adjustment or process re-validation.
Addressing critical commercial, technical, and quality control questions raised by enterprise buyers.
Connect directly with our senior formulation scientists and international procurement team for custom formulation quotes, technical specifications, and sample requests.
Get Catalog

