


Directly sourced, lab-tested, and manufactured under US FDA-registered & FSSC 22000 certified cleanrooms. Ready for global bulk supply and private-label scaling.
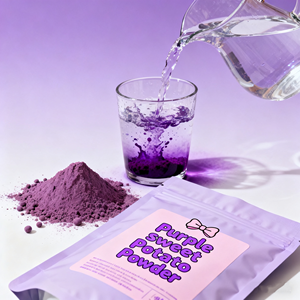
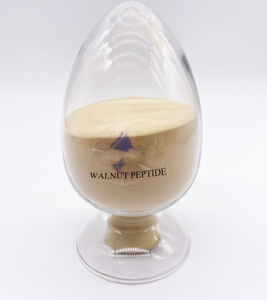
The global functional food, beverage, and nutraceutical raw material landscape is undergoing a systemic transformation. Supply chain managers, formula developers, and corporate procurement directors are migrating away from unstandardized raw powders toward high-efficacy, enzymatically processed bioactives, clinically validated peptides, and non-GMO functional carriers. Drivers such as tightening US FDA NDI (New Dietary Ingredient) requirements, EU Novel Food regulations, and stringent EFSA safety assessments have elevated the bar for raw material suppliers worldwide.
As brand owners struggle with consumer demands for clean-label declarations, thermal stability, and immediate bioavailability, modern OEM/ODM functional ingredient factories must offer more than commodity trading. Successful procurement strategies now prioritize suppliers with vertically integrated manufacturing infrastructure, full analytical traceability (HPLC, GC-MS, ICP-MS), and robust stability kinetic data across varying ambient conditions.
Protection of sensitive lipids (like Vitamin K2 MK7) against degradation caused by moisture, mineral interaction, and oxidative pressure during extended shelf life.
Shift toward small-molecule hydrolyzed peptides (<1000 Daltons) such as Walnut Bioactive Peptides for rapid intestinal transport and target organ delivery.
Replacement of synthetic binders with multifunctional prebiotic fibers like Isomalto-Oligosaccharide (IMO) and Ube extract to achieve zero-sugar label claims.
To optimize product performance and streamline formulation development, procurement teams must evaluate key functional parameters across primary ingredient categories. The matrix below outlines bio-activity markers, solubility profiles, and industrial dosage platforms.
| Functional Active | Standard Specification | Solubility / Processing Profile | Target Product Platform | Primary Regulatory Claim Area |
|---|---|---|---|---|
| Bulk Taurine Powder | Assay 99.0%–101.0% (USP/EP) | Highly Soluble (Cold Water) | Energy Drinks, Gummies, Effervescents | Metabolic Energy & Osmoregulation |
| Walnut Peptide Extract | Oligopeptide < 1000 Da (85%+) | Complete Dissolution, Heat-Stable | Nootropic Powders, RTD Liquids | Cognitive Support & Microcirculation |
| Vitamin K2 (MK-7) Bulk | 0.2% - 98% All-Trans HPLC | Lipid/Dispersible Micro-Powder | Softgels, Hard Capsules, Premixes | Bone Mineralization & Arterial Health |
| Tapioca IMO Fiber | Sugar Free, IMO Content > 90% | High Viscosity, Heat & Acid Resistant | Protein Bars, Confectionery, Powders | Prebiotic Digestive Health & Bulking |
| Artemisinin Powder | 98% Active Sesquiterpene Lactone | Ethanol/Lipid Soluble, Powder Blend | Dietary Capsules, Herbal Tinctures | Cellular Defense & Immune Regulation |
| Papaya Juice Powder | Enzymatically Active Papain Extract | Instant Water Dispersible | Sachet Powders, Skincare Drinks | Nutricosmetics & Proteolytic Digestion |
Building upon over 38 years of dedicated manufacturing expertise (Established 1987), our contract manufacturing operations deliver an integrated ecosystem spanning raw material synthesis, custom formulation R&D, pilot scaling, regulatory dossier packaging, and worldwide logistics.
Operating across specialized, state-of-the-art manufacturing campuses in Paonta Sahib (Himachal Pradesh) and corporate technical nodes in Noida (India), our production capability spans five core delivery platforms:
High-speed rotary presses producing up to 400 Million units/year. Capabilities include film coating, enteric coating, bilayer release, and effervescent technologies.
Automated hard-shell and liquid-fill encapsulation delivering 140 Million units/year under low-moisture control for sensitive probiotic and botanical active blends.
High-capacity fluid bed dryer and ribbon blender lines processing 35,000 Metric Tons/year of specialized sports nutrition, meal replacements, and fiber blends.
Fully automated filling lines yielding 70 Million units/year of botanical syrups, pediatric drops, and liquid nutritional shots.
Dedicated high-protein diskette and baked functional bite lines supplying 100 Million units/year for medical and therapeutic nutrition programs.
Serving brand partners across 60+ international countries with comprehensive COAs, Stability Protocols (ICH guidelines), and customized packaging.
Regulatory Compliance Standards: Facilities operate strictly under US FDA registration, Intertek-certified FSSC 22000, WHO-GMP, HACCP, ISO 22000, FSSAI, AYUSH (Ayurvedic Licensing), and Halal certifications. Complete technical documentation packages (Free Sale Certificates, Certificate of Analysis, Heavy Metal & Pesticide Residue Screening) are provided for seamless customs clearance.
Our in-house R&D innovation center is staffed by senior food technologists, pharmaceutical formulation scientists, and regulatory experts. Over 850 commercialized SKUs have been successfully engineered, scaled, and distributed worldwide. We partner with pharmaceutical multinationals, direct-to-consumer (D2C) nutrition leaders, and retail brand owners at every phase of the product lifecycle:
Connect directly with our technical procurement engineering team to request sample kits, analytical COAs, tier-pricing structures, or custom OEM formulation estimates.