Engineered to comply with Australian TGA labeling standards, humidity protection, and shelf-life durability for Melbourne importers and brand owners.
Melbourne has firmly established itself as Australia’s primary epicenter for wellness innovation, sports nutrition D2C startups, and boutique complementary medicine brands. From the vibrant health-conscious retail hubs of Fitzroy, South Yarra, and Richmond to the major pharmaceutical distribution corridors along Port Melbourne and Dandenong, Victorian consumers demand uncompromised product purity, aesthetic elegance, and strict environmental accountability.
For Australian supplement brand owners, contract manufacturers, and procurement directors, sourcing rigid containers, effervescent cylinders, and bespoke packaging boxes from leading Chinese exporters is no longer just a cost-efficiency decision—it is a strategic supply-chain advantage. However, navigating the intersection of **Therapeutic Goods Administration (TGA)** packaging guidelines, **Australian Packaging Covenant Organisation (APCO)** 2025 recycled material mandates, and climate-induced barrier requirements requires an expert packaging partner with deep engineering capabilities.
Our OEM/ODM manufacturing campus bridges Chinese high-volume precision manufacturing with Australian localized market expectations. By integrating US FDA-registered cleanroom extrusion, FSSC 22000 food safety management systems, and specialized pharmaceutical-grade QA protocols, we deliver export-ready containers engineered specifically to survive ocean freight to the **Port of Melbourne** while commanding premium shelf appeal at retail.
To assist procurement managers and quality assurance teams in selecting the optimal dosage packaging format, the technical evaluation matrix below outlines the moisture vapor transmission rates (MVTR), UV degradation protection, recyclability ratings, and TGA compatibility for primary materials used across our product line:
| Material / Container Type | MVTR Barrier (g/m²/day) | UV Shielding Capacity | TGA / FDA Compliance | APCO Recyclability | Recommended Application |
|---|---|---|---|---|---|
| Polypropylene (PP) Effervescent Tubes | < 0.05 (Airtight + Desiccant) | Moderate (Opaque White) | Pharma Grade 100% Pass | RIC #5 - Fully Recyclable | Effervescent Vitamin C, Electrolytes, Hydration Tabs |
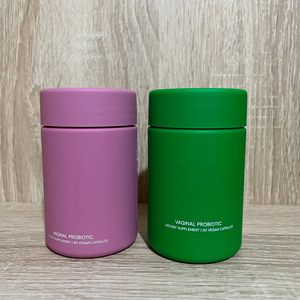
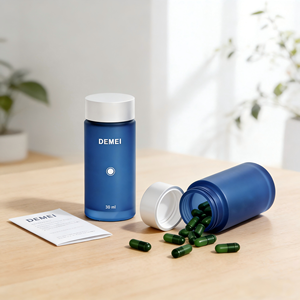
| HDPE Soft-Touch Matte Bottles | < 0.12 (High Barrier) | High (Colored / Opaque) | US FDA 21 CFR 177.1520 | RIC #2 - High Recycling Value | Clinical Softgels, Herbal Extracts, Multivitamins |
| Amber & Frosted PET Jars | < 0.45 (Standard Moisture) | High (Amber / Cobalt Blue) | Food-Contact Grade Certified | RIC #1 - Kerbside Preferred | Botanical Capsules, Nootropic Powders, Gummies |
| Type III Pharmaceutical Glass Jars | 0.00 (Absolute Gas/Moisture Barrier) | Maximum (99.8% UV Block) | Pharma Class A Standard | Infinite Circular Recyclability | Luxury Anti-Aging Probiotics, Premium Marine Collagen |
| Eco Kraft Paperboard Tubes | N/A (Requires Inner Foil Lining) | 100% Light Exclusion | FSC & Food Grade Lined | Biodegradable Outer Shell | Organic Protein Powders, Vegan Superfood Blends |
Every suburb and market sector in Melbourne exhibits unique consumer preferences and distribution demands. We design our packaging platforms to address specific localized application scenarios:
Melbourne’s active cycling and sports community along the Bay Trail and Albert Park demands convenient, moisture-proof hydration solutions. Our PP Cylinder Effervescent Tablet Tubes feature integrated silica gel caps that actively absorb ambient humidity, preventing premature tablet degradation during Melbourne's unpredictable weather transitions.
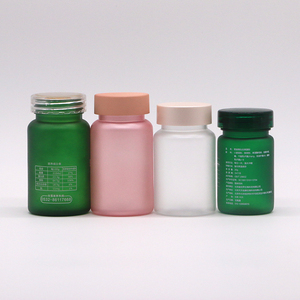
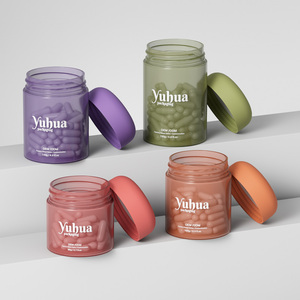
D2C wellness brands targeting aesthetic-conscious consumers in Fitzroy require luxury, tactile packaging. Our Matte Frosted PET & Glass Jars with custom translucent color tints offer a sleek, minimalist aesthetic that elevates shelf presence, increases unboxing delight, and reinforces premium brand positioning.
Products supplied to major Australian pharmacy retailers (Chemists Warehouse, Priceline) must meet stringent safety protocols. Our HDPE Soft-Touch Pill Bottles are engineered with certified Child-Resistant Closures (CRC) and tamper-evident induction heat seal liners, fulfilling TGA therapeutic packaging criteria.
The Australian health supplement packaging sector is undergoing a rapid evolution driven by changing environmental legislation and consumer behavior. Key trends shaping Victorian buying behavior include:
With Australia’s National Packaging Targets mandating higher recycled content, Victorian brands are prioritizing 30% to 100% rPET and rHDPE containers. Our facility provides certified food-grade PCR resins that maintain crystal-clear transparency or rich opaque colors without sacrificing structural tensile strength or barrier properties.
Glossy plastic bottles are increasingly perceived as legacy pharma packaging. Modern Australian D2C brands are shifting toward soft-touch rubberized coatings and frosted matte finishes. This visual and tactile differentiation conveys clean-label sophistication and premium formulation quality.
Exporting finished Australian supplements back into Asian markets requires robust anti-counterfeiting measures. We support advanced packaging integration including high-resolution QR code laser etching, tamper-evident security foil seals, and serialised batch tracking print surfaces.
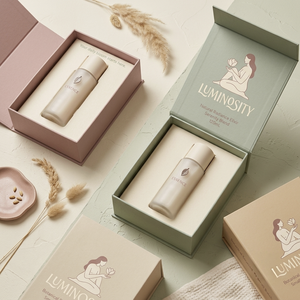
Sustainability-minded Melbourne brands are utilizing 100% recyclable paperboard tube boxes for secondary packaging of collagen bottles and powdered drink mixes. Our custom magnetic rigid paper packaging provides an ultra-luxury presentation for high-value gift sets and subscriber kits.
Built upon a legacy of precision engineering, our manufacturing infrastructure serves as a trusted contract manufacturing and specialized packaging hub for global nutraceutical and pharmaceutical giants across 60+ countries.
Our production facilities operate under strict US FDA registration, Intertek-certified FSSC 22000, GMP, and ISO systems. Automated blow-molding and injection molding take place in 100,000-class cleanrooms to prevent airborne particulate contamination.
Every production batch undergoes rigorous instrumented testing—including HPLC, gas chromatography, microbial limits, leak testing under vacuum pressure, and stability testing chambers to guarantee zero defects upon arrival in Australia.
From initial 3D digital rendering and prototype rapid sampling to custom mold building and high-speed multi-cavity production, our in-house engineering team shortens product development cycles from months to weeks.
Addressing key logistics, regulatory, and technical queries for seamless importing into Victoria.
All materials used (HDPE, PET, PP, Glass, Silicone seals) are 100% virgin food-contact grade or certified food-grade PCR resins compliant with US FDA 21 CFR standards and European Pharmacopoeia specifications. This ensures complete non-leachable safety when submitting regulatory dossiers to Australia’s Therapeutic Goods Administration (TGA). Furthermore, our plastics fall cleanly into APCO kerbside recycling categories (RIC #1, #2, and #5).
Direct ocean sea freight from our primary port export hubs (Ningbo / Shanghai) to the Port of Melbourne typically takes between 14 to 18 days in transit. Standard production turnaround for custom container orders ranges from 20 to 30 days depending on customization complexity (custom color matching, hot stamping, or soft-touch coating). Emergency air freight options are also supported via Melbourne Airport (MEL).
Yes. We provide precise Pantone color-matching for bottle bodies, caps, and closures. We support a wide spectrum of surface treatments including matte frosted spray coating, soft-touch rubberized tactile finishes, metallic UV electroplating, and custom silk-screen or hot-foil stamping artwork. Standard neck finishes include 33-400, 38-400, 45-400, and custom child-resistant thread profiles.
We offer ISO 8317 and US CPSC-certified Child-Resistant (Push-Down & Turn) caps suitable for high-potency formulations. Tamper evidence can be achieved via tear-off bands on effervescent tubes, shrink sleeves, or induction heat-seal aluminum foil liners engineered to bond cleanly with HDPE, PET, or glass container rims.
Our standard MOQ for stock color containers starts as low as 3,000 to 5,000 units. For custom Pantone color matching, specialized soft-touch coatings, or custom-printed magnetic rigid paper boxes, MOQs typically range from 10,000 to 20,000 units, allowing scaling D2C brands in Melbourne to maintain lean inventory cycles.
Absolutely. We dispatch rapid 3D-printed prototypes or actual molded physical samples with your custom branding artwork and color specifications via DHL/FedEx express directly to your Melbourne office or contract packing facility for line trial testing and sign-off.
Request technical material datasheets, physical sample kits, or immediate factory-direct wholesale pricing for your next packaging order.