Precision-blended, cGMP-manufactured nutrient compounds designed for seamless integration into human foods, animal feeds, pharmaceuticals, and functional beverages in the Boston region.
The Greater Boston region—encompassing Kendall Square, the Route 128 tech corridor, and extended New England manufacturing hubs—stands as one of the world's most dense concentrations of life science innovation, clinical research, and advanced functional food start-ups. In this environment of rigorous analytical standards, procuring custom vitamin premixes is no longer merely a purchasing decision; it is a critical bio-engineering alignment. Local pharmaceutical developers, RTD (Ready-to-Drink) beverage pioneers, and commercial livestock integrators require premix partners who can deliver batch-to-batch homogeneity, strict particle size management, and full US FDA compliance.
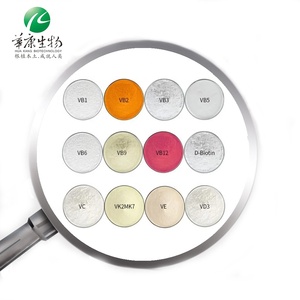
Vitamin premixes serve as complex multi-component matrices where fat-soluble vitamins (A, D3, E, K1/K2) and water-soluble compounds (Thiamine B1, Riboflavin B2, Niacin B3, Pyridoxine B6, Folic Acid B9, Cyanocobalamin B12, and Vitamin C) are combined with essential trace minerals (Zinc, Iron, Selenium, Copper, Manganese, Chromium). Achieving thermodynamic stability across these varied chemical profiles requires advanced micro-encapsulation, spray-drying, and fluid-bed granulation techniques. Without engineered particle coating, reactive trace elements like ferrous sulfate or cupric sulfate can accelerate oxidation of delicate vitamins like A and C, leading to shelf-life degradation and off-flavors.
Protects heat- and light-sensitive vitamins against oxidation during thermal processing, pasteurization, or extended storage in humid environments.
Custom milling and sifting (80 to 100 mesh) ensures zero segregation during high-speed dry blending, tableting, or continuous liquid batch tank dosing.
High-Performance Liquid Chromatography (HPLC) and Mass Spectrometry testing ensure targeted potencies account for manufacturing stress overages.
To assist Boston-based procurement teams, food scientists, and formulation experts, the matrix below details the technical specifications across key vitamin and mineral premix categories:
| Application Sector | Active Components | Carrier / Matrix System | Solubility / Dispersion | Stability & Overages |
|---|---|---|---|---|
| Functional RTD Beverages | B-Complex (B1, B2, B3, B6, B12), Vit C, Zinc Citrate | Maltodextrin / Water-Soluble Fiber | Instant Clear Dissolution (<30s) | 10–15% overage; pH stable 2.8–6.5 |
| Nutraceutical Tablets & Capsules | Vitamins A, C, D3, E, Methylfolate, Chelated Minerals | Microcrystalline Cellulose (MCC) | Direct Compression Grade | Micro-encapsulated; 24-month shelf life |
| Medical & Clinical Foods | Complete RDA Micronutrient Profile + Amino Acids | Hypoallergenic Rice Starch / Acacia | Fine Suspension (80 Mesh) | Nitrogen flushed; low heavy metal assay |
| Livestock & Aquaculture Feeds | Vitamins A, D3, E, Choline Chloride, B-Vitamins, Trace Minerals | Distillers Dried Grains / Corn Cob Carrier | Dry Feed Mash / Pellet Dispersion | Thermal stability up to 90°C during extrusion |
From functional beverage incubators in South Boston to commercial agricultural operations in the Connecticut River Valley and New England dairy hubs, our vitamin premixes meet specific regional demands:
Greater Boston is a thriving innovation market for cold-pressed juices, sparkling wellness waters, and botanical energy drinks. Formulating beverages requires premixes that leave zero sediment, resist thermal degradation during pasteurization, and maintain clarity. Our water-dispersible B-complex and vitamin C premixes feature specialized particle sizing and pH-adjusted buffer systems tailored for acidic beverage matrices.
With regional dietary supplement brand headquarters operating across Massachusetts and Connecticut, contract manufacturers demand directly compressible (DC grade) premixes. We supply custom vitamin-mineral blends optimized for high-speed tablet presses and capsule filling lines, preventing cap separation, weight variation, and machine binding.
Partnering with institutions affiliated with Boston’s world-renowned medical centers, our production blocks manufacture ultra-pure, elemental vitamin premixes for enteral nutrition, geriatric supplements, and metabolic recovery formulas. Every batch undergoes stringent microbial testing, endotoxin screening, and heavy metal assays.
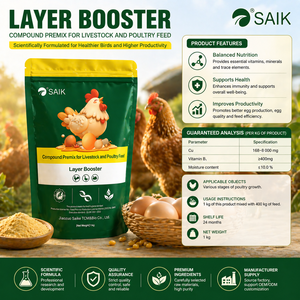
New England’s agricultural producers require robust feed-grade premixes to maintain livestock immunity, improve layer hen shell quality, and optimize growth efficiency. Our specialized lines—such as SAIK Layer Boosters, RUIPU 10% Folic Acid powders, and Choline Chloride corn cob premixes—provide high stability during feed pelleting and extrusion processes.
Procurement managers and brand strategists in New England are navigating rapidly shifting regulatory and consumer expectations. Understanding these localized growth drivers ensures long-term market competitiveness:
Consumers in the Northeast aggressively favor transparent ingredient decks. Demand has shifted away from synthetic excipients and carrier bases toward non-GMO maltodextrin, organic rice concentrate, and acacia gum. Our R&D center provides custom carrier substitution without sacrificing powder flowability.
Boston’s research-savvy demographic prefers active vitamin forms over synthetic precursors—such as L-5-Methyltetrahydrofolate (L-5-MTHF) over standard Folic Acid, and Methylcobalamin over Cyanocobalamin. We specialize in bio-identical vitamin premix integrations.
Post-logistics bottlenecks have prompted Boston buyers to demand guaranteed delivery cadences via I-95/I-90 logistics hubs. Working with established global facilities offering regional staging ensures rapid order fulfillment and continuous manufacturing uptime.
Leveraging over 38 years of pharmaceutical and nutraceutical contract manufacturing heritage, our partner production hubs operate under strict cGMP guidelines, holding accreditations from US FDA, FSSC 22000 (Intertek certified), ISO systems, HACCP, FSSAI, AYUSH, and Halal bodies.
Equipped with specialized blocks producing up to 400M tablets, 140M capsules, 70M oral liquids, 100M nutritional diskettes, and 35,000 MT of powders annually.
In-house laboratories utilize High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC), Atomic Absorption, and microbiology suites for thorough batch release.
Environmentally controlled production suites maintain ultra-low relative humidity to prevent hygroscopic vitamin clumping and preserve strain viability in probiotic-vitamin blends.
Clear, technical answers to common queries regarding compliance, order quantities, custom formulations, and regional shipping timelines.
Every shipment is accompanied by a full Certificate of Analysis (CoA) detailing active assays via HPLC/UV methods, heavy metals (Pb, Cd, Hg, As), microbial counts (TPC, Yeast & Mold, E. coli, Salmonella), bulk density, particle mesh size, and loss on drying. Additionally, US FDA registration numbers, FSSC 22000 certificates, Allergen Declarations, Non-GMO statements, and BSE/TSE-free guarantees are provided for smooth audit verification under 21 CFR Part 111 / Part 117.
Yes. Our R&D team works directly with beverage scientists to create tailored vitamin-mineral premixes aligned with specific target pH levels, flavor systems, thermal processing profiles (HTST, UHT, Retort), and clarity specs. We incorporate solubility enhancers, acidity regulators, and maskers to ensure optimal taste and appearance without cloudiness or precipitation.
We utilize advanced micro-encapsulation techniques where fat-soluble nutrients are emulsified in a protective matrix (such as food starch, gelatin, or gum arabic) and spray-dried into beadlets. Antioxidants like Tocopherols or Sodium Ascorbate are incorporated directly into the beadlet wall, preserving vitamin potency over a 24-month shelf life even when blended with reactive minerals.
Standard MOQs for custom premix formulations start at 500 kg to 1,000 kg depending on raw material active profiles. For standard catalog items, lower MOQs are available. Prototype development and pilot batch formulation take approximately 2–3 weeks, followed by commercial manufacturing and delivery to Massachusetts logistics hubs in 4–6 weeks.
Our manufacturing suites utilize validated high-capacity V-blenders and double-cone blenders equipped with intensifier bars. Raw materials undergo micronization and pre-sifting to match particle sizes prior to blending. In-process sampling is conducted at multiple blender geometric points to confirm homogeneity (RSD < 2.0%) before final packaging into moisture-barrier aluminum foil liners and fiber drums.
Whether you are formulating a new functional beverage in Cambridge, scaling a dietary supplement brand in Boston, or sourcing high-potency livestock feed additives across New England—our engineering team is ready to support your technical specification requirements.
Get a Quote